

Bentonite pneumatic conveying solution
During the processing and transportation of bentonite powder, enterprises often face practical issues such as severe dust, pipeline blockages, high energy consumption, and frequent equipment maintenance. Traditional mechanical conveying methods easily cause material damage and lack of sealing, resulting in harsh workshop environments that affect production efficiency and employee health. How to achieve efficient, clean, and low-consumption conveying has become a key focus for the industry.
Material characteristics
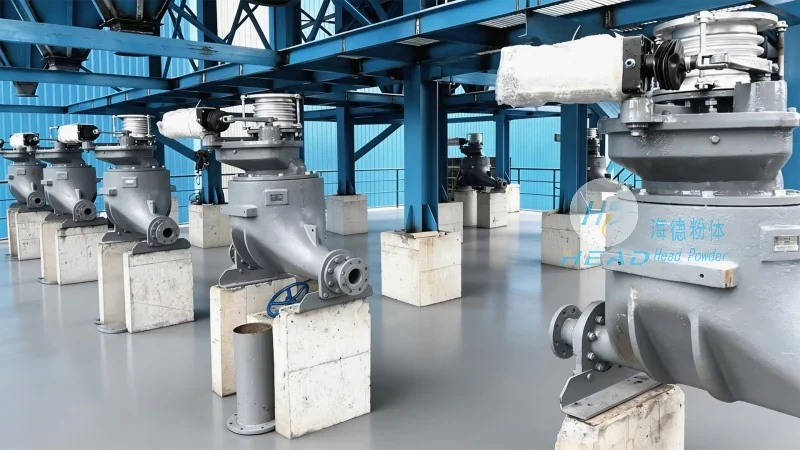
Bentonite is a clay mineral mainly composed of montmorillonite, characterized by high water absorption, expansiveness, cohesion, and thixotropy. They have fine particle size (usually above 200 mesh), low bulk density, average fluidity, and are prone to moisture absorption and caking, requiring high sealing and moisture-proof capabilities of conveying equipment. At the same time, the fluffy nature of the material means that excessive airflow speed during transportation must be avoided from excessive airflow speed, which could cause material breakage or pipeline wear.
Product Introduction
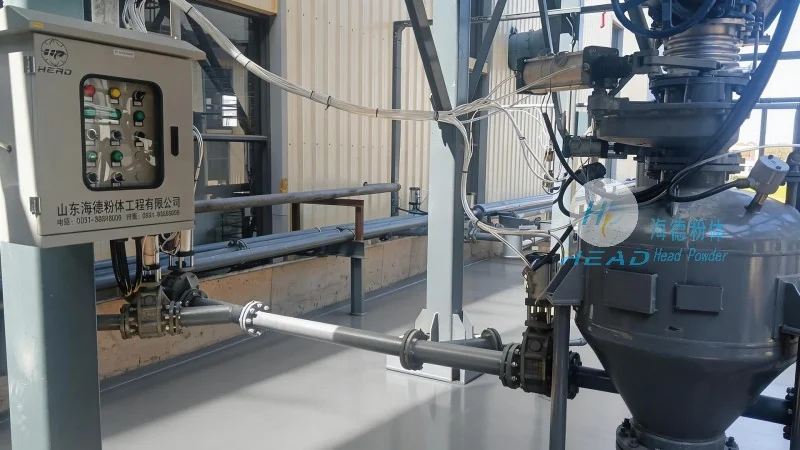
The bentonite pneumatic conveying system provided by Head Powder adopts the principle of dense phase transport under positive or negative pressure, specially designed for bentonite's tendency to absorb moisture and become clogged. The system consists of a feeding device, conveying pipelines, air source equipment, dust separation and removal device, and an automatic control system. It enables fully enclosed, automated conveying from the raw material silo to the point of use, effectively reducing dust spillage and lowering the intensity of manual intervention. Equipment materials can be selected based on the material's corrosiveness and wear resistance, using wear-resistant alloys or stainless steel to support continuous operation.
Product advantages
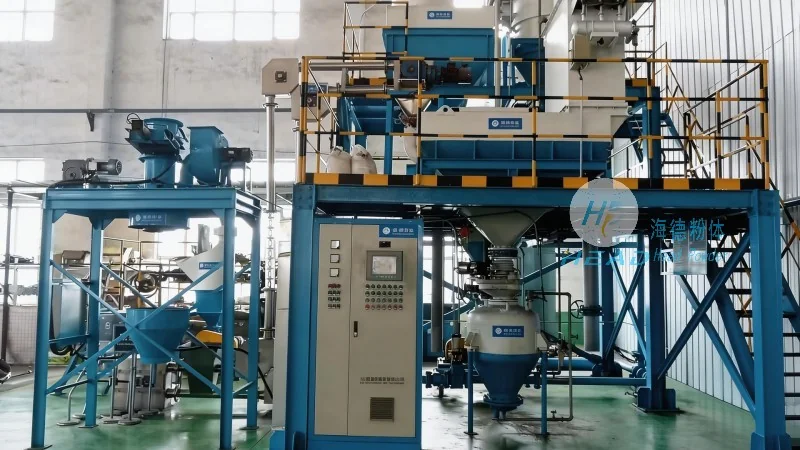
To address common customer concerns such as high dust generation, high energy consumption, and difficult maintenance, Head Powder offers the following solutions: the system uses low-flow dense phase conveying technology to reduce material damage and pipeline wear, while also lowering unit energy consumption; Equipped with intelligent pressure regulation and air volume control modules to adapt to different conveying distances and working conditions; Sealed pipelines combined with high-efficiency pulse baghouse dust collectors enable dust-free operation; The modular design facilitates maintenance, and the pipeline is equipped with anti-blockage purge interfaces, reducing downtime and cleaning time.