

Pneumatic Conveying Solution for White Sugar Powder
In the food processing and pharmaceutical industries, the transportation of powdered white sugar often faces practical issues such as material clumping, pipeline blockages, dust emissions, and cross-contamination. Traditional mechanical conveying methods not only have high maintenance costs but also struggle to meet the requirements of clean production environments. How to achieve efficient, sealed, and low-damage conveying of powdered white sugar has become a technical challenge that many enterprises urgently need to solve.
Material characteristics
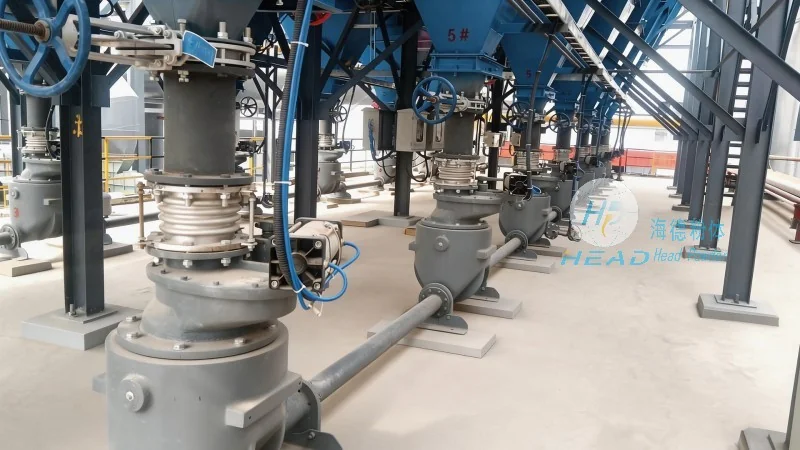
White sugar powder is a typical fine powder, with particle sizes typically ranging between 100~300 microns. It has strong hygroscopic properties, poor fluidity, easy clumping, and static electricity generated by friction. During conveying, if environmental humidity is not properly controlled, wall hanging and bridge erection are very likely, seriously affecting production continuity. In addition, powdered white sugar is sensitive to temperature; high temperatures may cause charring and discoloration, so the conveying system must balance moisture resistance, anti-caking effects, and temperature control requirements.
Product Introduction
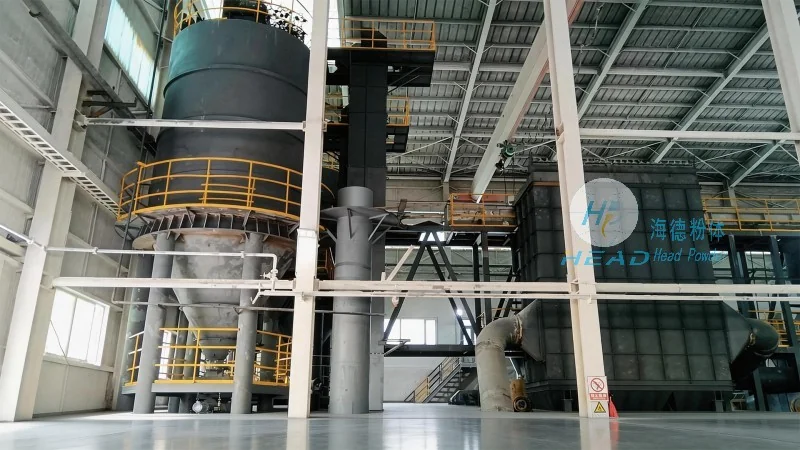
The pneumatic conveying system provided by Head Powder uses sealed pipeline positive or negative pressure conveying methods to smoothly deliver materials from the feeding end to each usage point. The system can be customized according to the customer's site layout, capacity requirements, and material characteristics, including feeding devices, conveying pipelines, gas source equipment, dust separation and removal devices, and automatic control systems. Core components are made from food-grade materials, with smooth surfaces that are easy to clean, meeting GMP and food safety and hygiene standards. The system operates smoothly, allowing materials to be conveyed in a sealed environment, effectively preventing the intrusion of external moisture and impurities, and reducing the risk of caking.
Product advantages
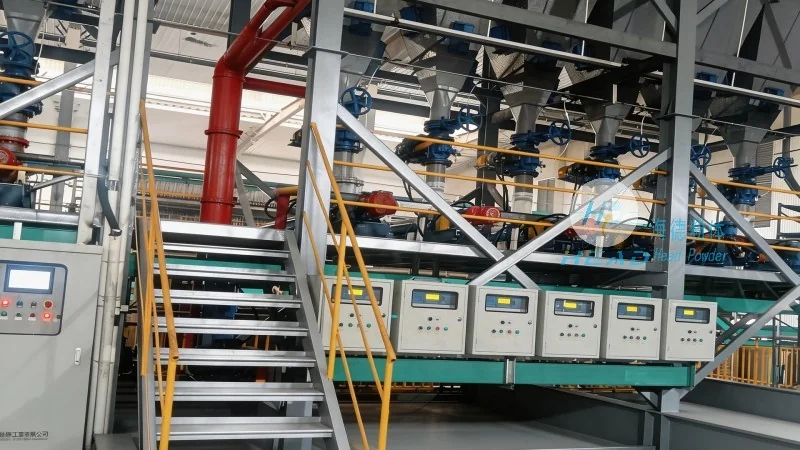
To address pain points such as sugar powder being prone to moisture absorption, clogging, and dust control, Head Powder Pneumatic Conveying Solution has the following features:
- Moisture-proof sealed design:The entire pipeline is sealed, combined with a dehumidifying air source, reducing moisture contact at the source, keeping materials dry, and preventing caking.
- Low Damage Conveying:Using low-speed, high-concentration or dilute phase conveying methods, with flow rate and gas-solid ratio adjusted according to material brittleness, helps maintain the integrity of powdered sugar granules.
- Intelligent Control:Integrated PLC automation system enables precise adjustment of conveying volume, automatic back-blowing of pipe blockages, fault alarms, and remote monitoring, reducing manual intervention.
- Clean and environmentally friendly:Equipped with high-efficiency filtration and dust removal devices, exhaust emission concentrations below industry standards, no dust emissions in the workshop, supporting the working environment and employee health.
- Flexible customization:Supports complex process requirements such as multi-point feeding, multi-product switching, and batch production, adapting to new production lines or retrofitting old equipment.
With years of powder conveying experience, Head Powder has provided stable and reliable pneumatic sugar powder conveying systems for many food and pharmaceutical companies, helping customers improve production efficiency, reduce operating costs, and meet increasingly stringent food safety standards.