

Pneumatic conveying solution for grain pellets
In the processing and storage stages of grain pellets, traditional mechanical conveying methods often face issues such as high material damage rates, severe dust pollution, restricted conveying routes, and frequent equipment maintenance. Especially in long-distance or complex spatial layouts, manual handling and belt conveying are not only inefficient but also prone to cross-contamination, increasing operational costs and safety risks for enterprises. How to achieve efficient, clean, and low-loss grain pellet transportation has become a common concern for the industry.
Material characteristics
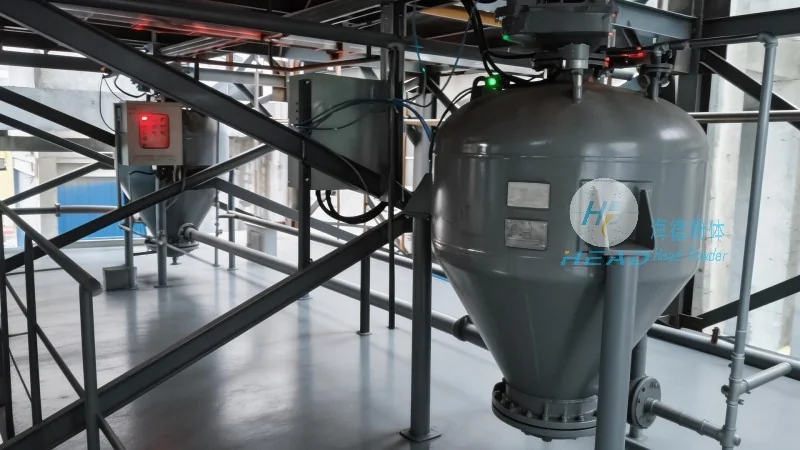
This solution targets common grain grains (such as rice, wheat, corn, soybeans, etc.). These materials have uniform particle size and moderate density, but their surfaces are relatively brittle, making them prone to breaking particles or powder during mechanical collisions; It also has typical hygroscopic absorption and tendencies for static electricity accumulation, with specific requirements for airflow speed, pipe material, and sealing during conveying. In addition, grain particles often contain dust, raising higher standards for environmental hygiene and explosion-proof safety.
Product Introduction
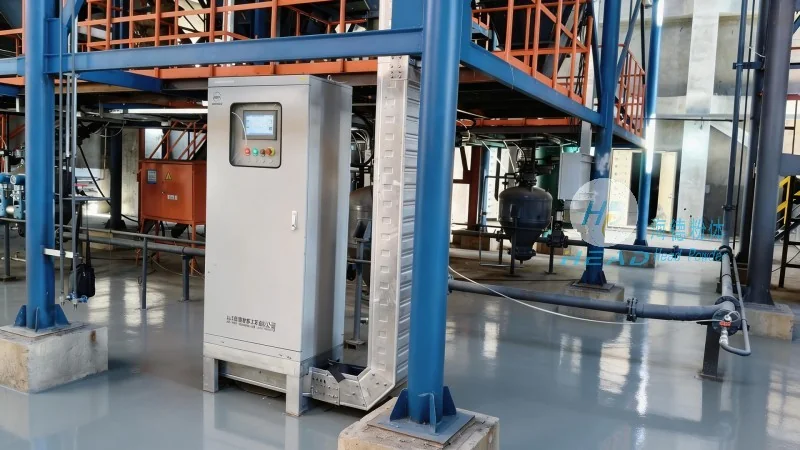
The pneumatic conveying solution for grain pellets provided by Head Powder is a sealed pipeline conveying system based on the principles of positive or negative pressure. The system consists of air source equipment (fans/air compressors), feeding devices, conveying pipelines, dust separation and removal units, and intelligent control systems. Tailored to the characteristics of grain particles, we use low-flow, high-density dilute or dense phase conveying modes, equipped with dedicated rotary valves or ejectors to help materials flow smoothly through pipelines. The complete set of equipment can be customized according to on-site process layout, conveying distance, and output requirements, suitable for scenarios such as grain storage, feed production, brewing, and food processing.
Product advantages
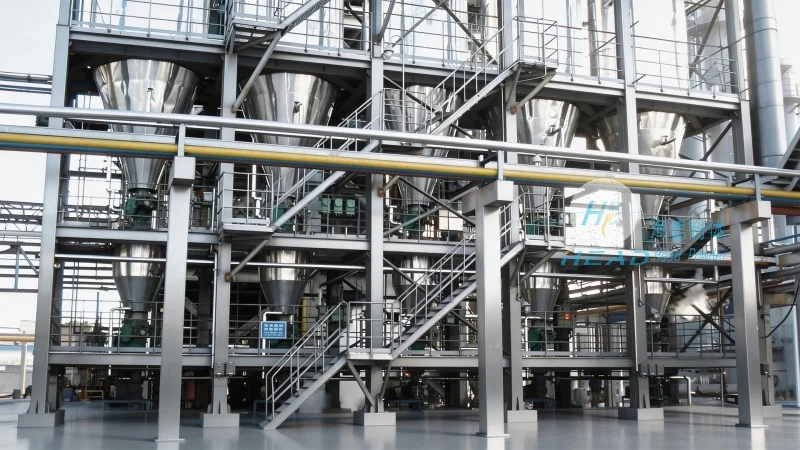
To address customer pain points, this solution achieves the following improvements:
- Low damage rate: By optimizing airflow velocity and feeding methods, collisions between particles and between particles and the pipe wall are reduced, with a crushing rate over 60% lower than traditional mechanical conveying.
- Sealed tightly and free of dust: Fully enclosed pipeline system combined with high-efficiency dust collectors prevents dust leakage, meets environmental and hygiene requirements, and reduces the risk of dust explosions.
- Flexible layout: The pipeline can bend and climb freely along the building structure, without occupying ground space, easily crossing obstacles, and enabling multi-point, multi-line conveyance.
- Intelligent control: Equipped with PLC and sensors to monitor conveying volume, air pressure, and energy consumption in real time, automatically adjust operating parameters, reduce manual intervention, and enhance stability.