

Long-distance limestone powder conveying system in Wuhai, Inner Mongolia
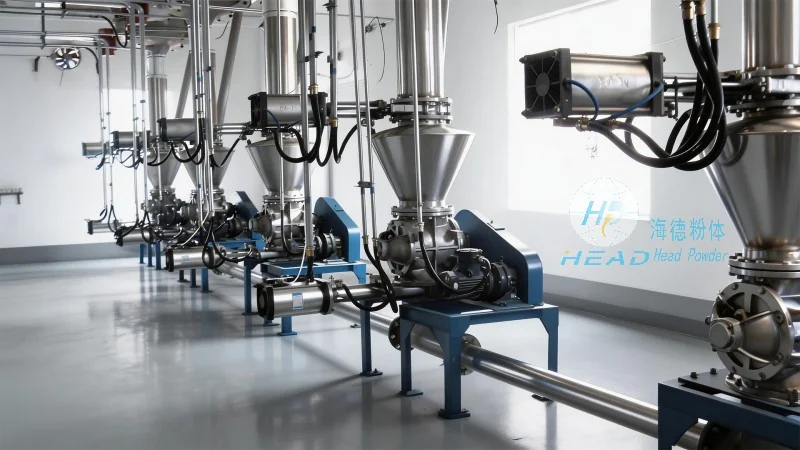
The long-distance limestone powder conveying system in Wuhai, Inner Mongolia, was designed and implemented by Head Powder commissioned by a certain company. This project aims to solve the long-distance, high-efficiency, and low-loss transportation of limestone powder from the mine to the production line, meeting the factory's demand for continuous and stable raw material supply.
Customer pain points
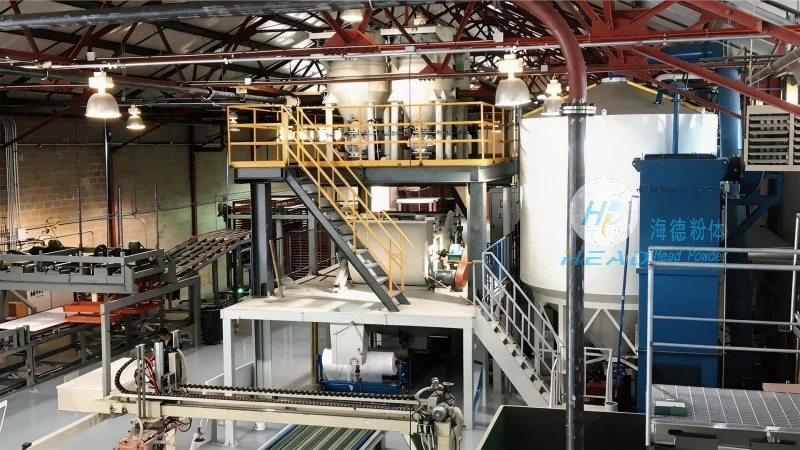
Customers face the following challenges in the traditional limestone powder conveying:
- Conveying distances can reach several kilometers, traditional mechanical conveying equipment occupies large space, requires high investment, and requires frequent maintenance;
- Limestone powder easily generates dust, causing environmental pollution and material loss, and does not meet environmental protection requirements;
- Equipment has high operating energy consumption, and daily operating cost pressures are significant;
- During conveying, blockages easily occur, affecting production continuity and causing output losses due to maintenance downtime.
Product advantages
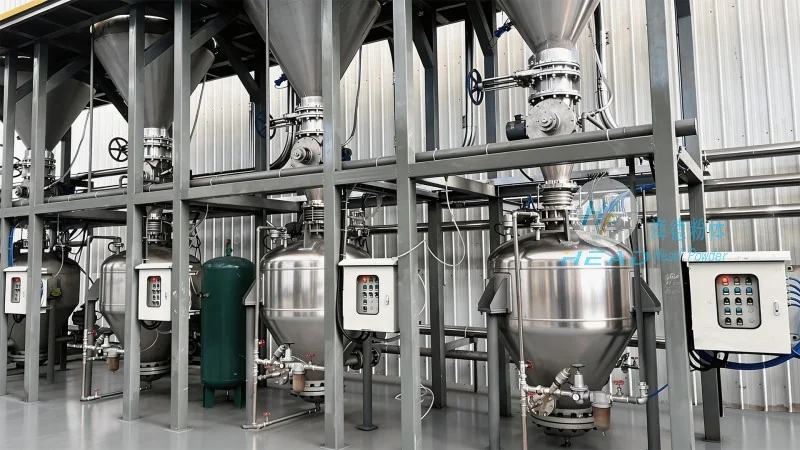
To address these pain points, Head Powder offers a fully enclosed pneumatic conveying system solution, adopting positive pressure concentrated phase conveying technology to achieve long-distance, high-flow, and low-energy-consumption stable transport of limestone powder. The system has the following features:
- Long-distance conveying capability: A single pipeline can meet requirements for distances of several kilometers, eliminating the need for intermediate transfers and reducing equipment investment;
- Sealed and dust-free operation: The entire system is sealed to prevent dust leakage, meet environmental standards, and reduce material loss; li>
- Low energy consumption and high efficiency: By optimizing air source matching and delivery parameters, unit energy consumption is reduced by more than 20% compared to traditional methods;
- Intelligent control: Equipped with an automated monitoring system to adjust conveying status in real time, effectively preventing pipe blockages and supporting production continuity.
Currently, this system has been operating normally for many years, helping customers achieve dual improvements in clean production and economic benefits.