

Complete set of explosion-proof pneumatic conveying of silicon powder in Xuchang, Henan
Head Powder successfully implemented a complete explosion-proof pneumatic conveying project for silicon powder in Xuchang, Henan, providing a systematic solution to the safety and efficiency challenges in powder material transportation. This project adopts closed-circuit conveying and intelligent monitoring technology to achieve safe, sealed, and efficient transfer of silicon powder, effectively avoiding dust explosion risks and helping customers improve production stability and environmental compliance.
Project Background
A chemical company has long faced dust leakage and explosion hazards during silicon powder transportation. Traditional mechanical conveying methods are not only inefficient but also create potentially explosive atmospheres in the working environment due to the fine particle size of silica powder and dust generation, posing ongoing threats to factory safety. At the same time, existing equipment suffers from severe wear and high maintenance costs, making it difficult to meet increasingly stringent safety production and environmental protection standards.
Customer pain points
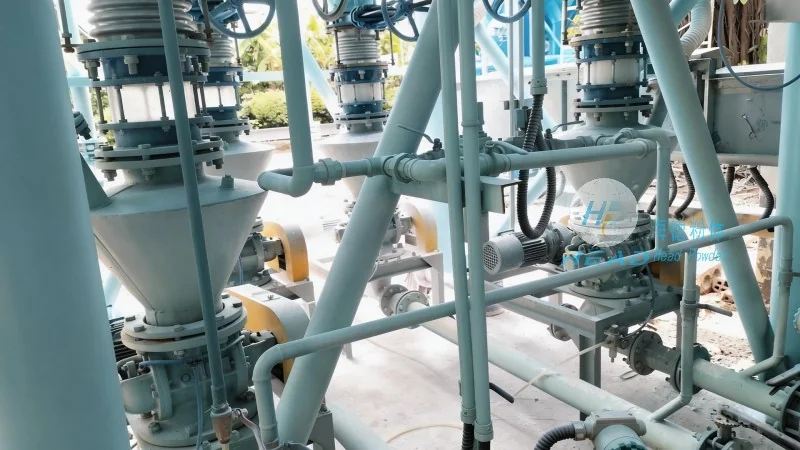
The company faces three core pain points in the silicon powder transportation process: First, the high risk of dust explosions and the lack of effective explosion-proof design and proactive protection measures; Second, poor sealing during conveying, material leakage leads to raw material waste and workshop environmental pollution; Third, the system has a low degree of automation, relies on manual operation, and has slow fault response. Overall operational efficiency urgently needs improvement.
Head Powder Solutions
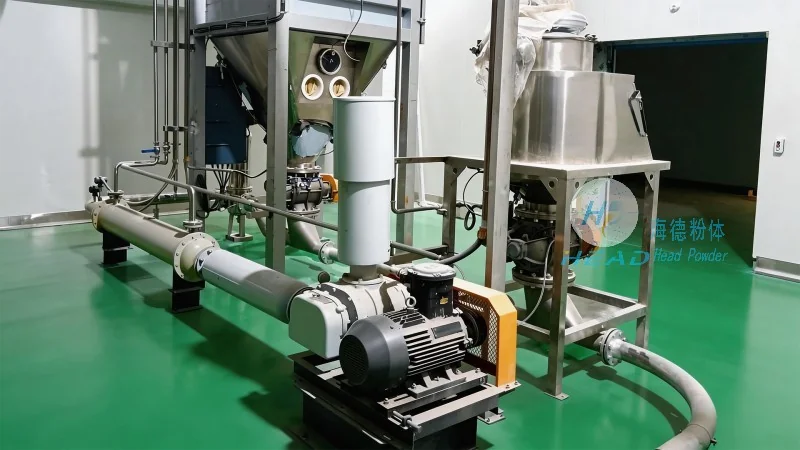
To address these pain points, Head Powder designed and delivered a complete silicon powder explosion-proof pneumatic conveying project. Core measures include: using a positive pressure dilute-phase pneumatic conveying system, combined with explosion-proof valves, explosion relief devices, and electrostatic grounding networks to eliminate ignition sources and explosion conditions at the source; The entire system uses sealed pipelines and negative pressure dust collection devices to achieve zero leakage material transportation; Integrated PLC automatic control system monitors parameters such as pressure, temperature, and flow in real time; automatically alarms and executes safety interlock actions in case of abnormalities, supporting continuous operation.
Project Results
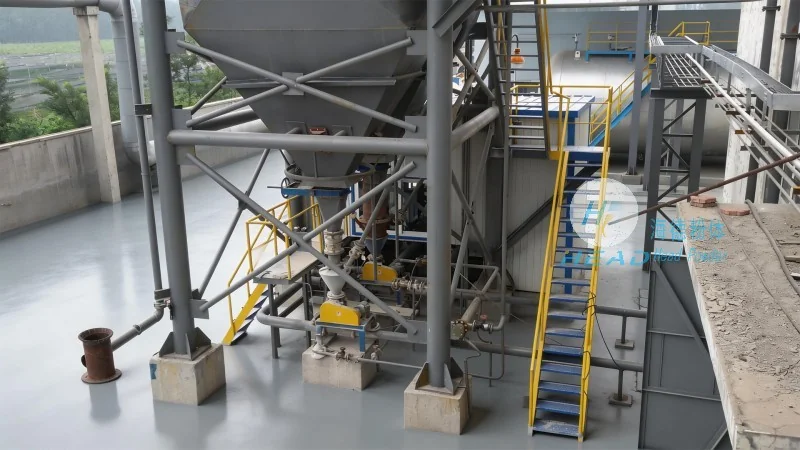
After the project was put into use, the dust emission concentration at the customer's factory dropped below the national limit, significantly improving the on-site working environment; Conveying efficiency improved by about 30% compared to original equipment, and equipment failure rates dropped by over 70%; The system operates stably, with no safety incidents caused by dust, and users fully recognize Head Powder's professional delivery capabilities.