

Pneumatic conveying solution for rare earth oxide powder
During the transportation of rare earth oxide powders, companies often face challenges such as dust leakage, material loss, equipment wear, and insufficient automation. These pain points not only affect the cleanliness of the production environment but also increase operating costs and maintenance difficulties. To address these challenges, Head Powder offers customized pneumatic conveying solutions for rare earth oxide powders, helping enterprises achieve efficient, clean, and stable material flow.
Material Characteristic Analysis
Rare earth oxide powders typically feature fine particles, low density, easy lifting, and strong hygroscopicity. Some materials also exhibit common corrosiveness or abrasive properties, placing high demands on the sealing, wear resistance, and moisture resistance of conveying equipment. Therefore, when designing the conveying system, factors such as material fluidization, bulk angle, and particle size distribution must be fully considered to ensure smooth pipeline delivery and reduce blockage.
Product Introduction
Head Powder's developed rare earth oxide powder pneumatic conveying system uses sealed pipeline conveying methods of positive or negative pressure, safely and accurately transferring powder from the feeding point to downstream process sections. The system is equipped with dedicated feeders, air supply equipment, pipeline components, dust removal devices, and intelligent control modules, allowing for non-standard customization based on customer site conditions, production requirements, and material characteristics. The entire set of equipment is compact in structure, easy to install, and can adapt to workshop space constraints and process changes.
Product advantages
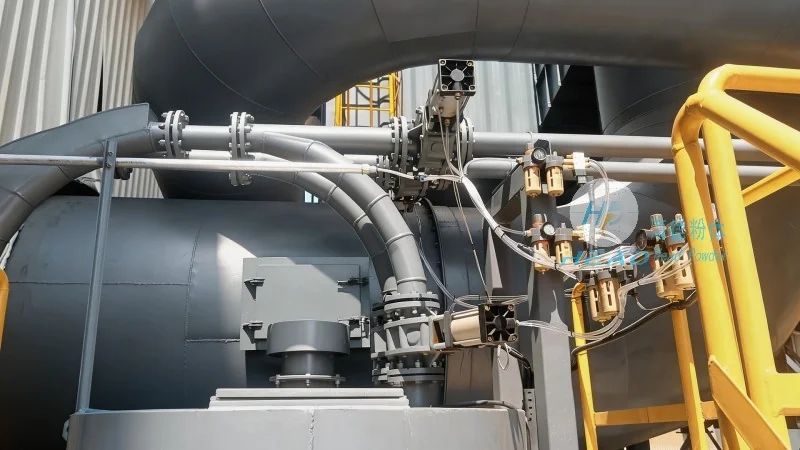
To address customer pain points, this conveyor system offers the following solutions:
- Fully enclosed conveying:The entire process from feeding to discharge is sealed, effectively suppressing dust leakage, improving the working environment, and reducing material loss.
- Low wear design:Combining fluidized feeding with low-speed conveying reduces friction between materials and pipe walls, extending equipment service life.
- Automatic control:Equipped with PLC and touchscreen, it can monitor conveying pressure, flow, and material blockage alarms in real time, supporting remote operation and reducing manual intervention.
- Flexible customization:Selecting suitable pipe materials (such as stainless steel or ceramic linings), seals, and gas source methods for different rare earth oxides can help ensure normal system operation.
Product features
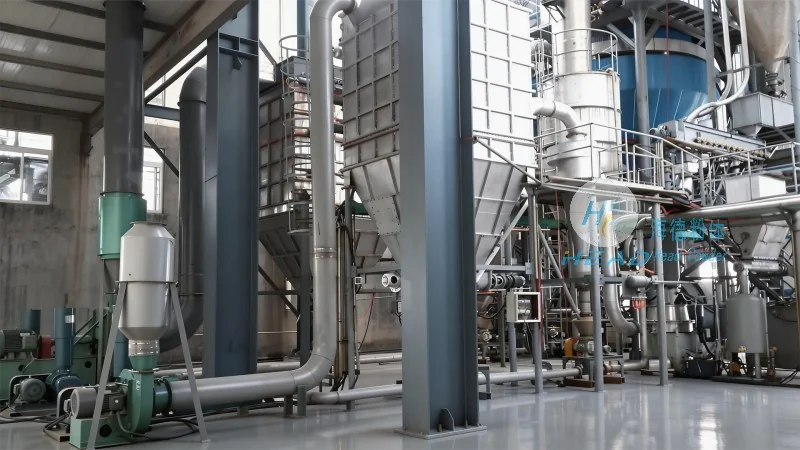
- Airtight and dust-free:The system uses sealed pipeline conveyance, combined with a high-efficiency dust removal and filtration device, ensuring no dust leakage in the workshop and meeting environmental protection requirements.
- Low Energy Consumption:Optimized air-solid ratio and air source configuration reduce compressed air consumption and lower long-term operating costs.
- Easy-to-maintain structure:Wear-prone parts such as feeders and elbows use quick-release designs for easy daily inspection and replacement, shortening downtime.
- Moisture-proof and anti-clumping:Optional heating or drying air sources can be provided to prevent moisture-absorbing materials from clumping inside the pipes and to ensure smooth conveying.
Technical specifications
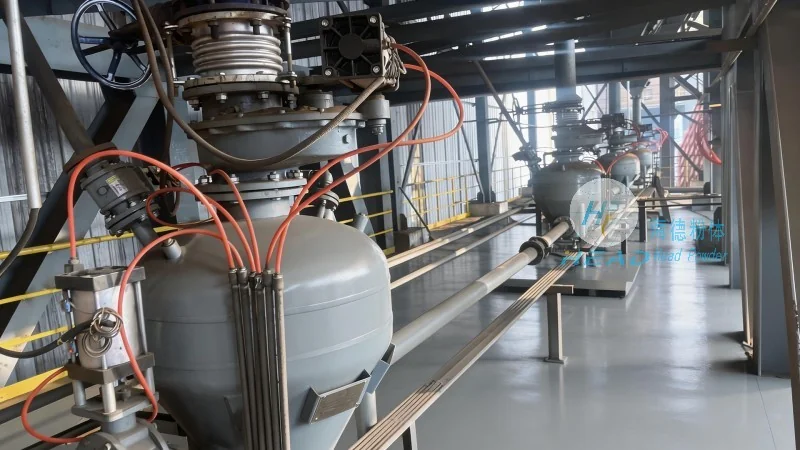
| Conveying capacity | 0.5~20 t/h (customizable) |
| Conveying distance | Horizontal ≤ 100 m, vertical ≤ 30 m |
| Work pressure | -0.08~0.8 MPa (selected according to conveying method) |
| Types of air sources | Roots blowers, air compressors (optional) |