

Shaanxi Yulin Rubber Powder Negative Pressure Dilute Phase Conveying Project
In the field of rubber powder conveying, a company recently completed a negative pressure dilute phase conveying project for rubber powder in Yulin, Shaanxi. This case fully demonstrates the practical value of negative pressure dilute phase technology in powder processing, providing customers with a stable and efficient conveying experience.
Case Summary
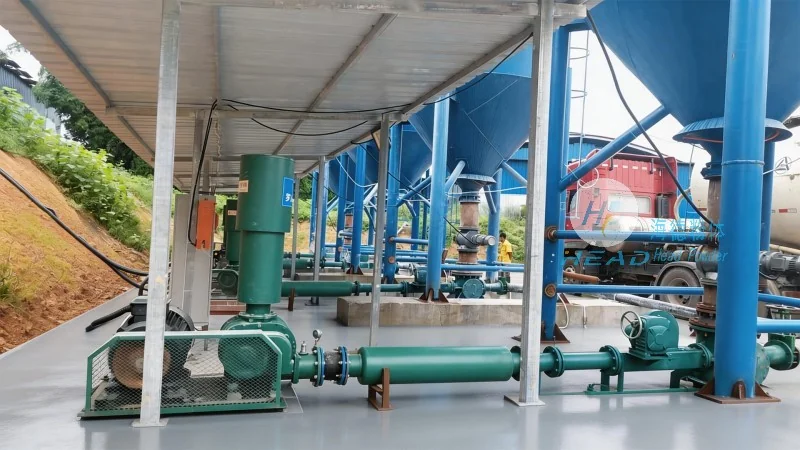
The project is implemented in Yulin, Shaanxi. To meet the material conveying needs of a customer's rubber powder production line, a company provided a complete negative pressure dilute phase conveying system. This system enables automated powder conveying through sealed pipelines, solving many problems faced by traditional conveying methods and is now operating normally at customer sites.
Customer pain points
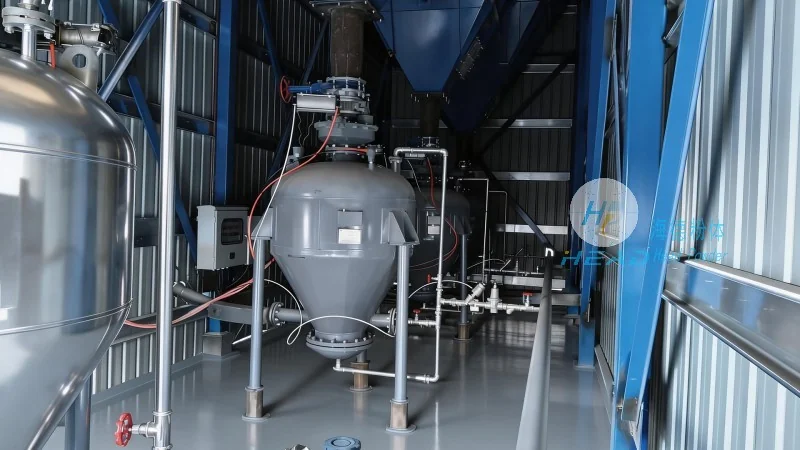
The customer faces the following main issues during rubber powder transportation: First, materials tend to generate large amounts of dust during transport, polluting the workshop environment and affecting workers' health; Second, traditional mechanical conveying equipment consumes high energy, making operating costs difficult to control; Third, frequent blockages in the conveyor pipelines have caused production line shutdowns for maintenance, affecting overall efficiency; Fourth, there is a lack of automated control methods, resulting in heavy manual operation and difficulty in improving conveying accuracy.
Product advantages
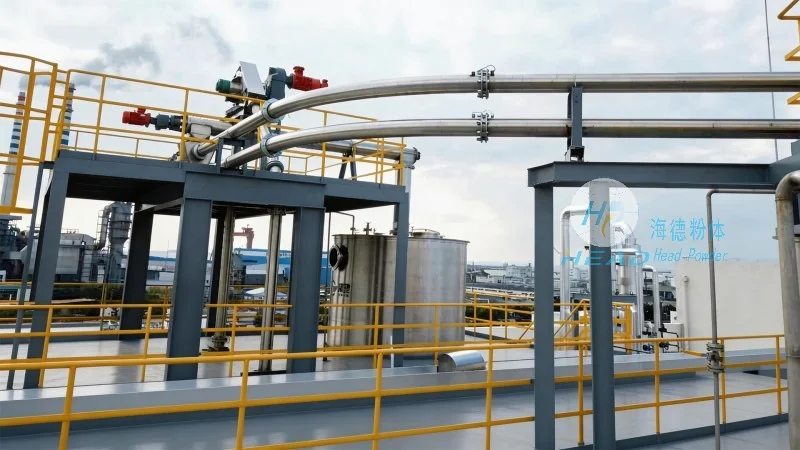
To address these pain points, a company provided a fully enclosed dilute phase conveying solution that prevents dust leakage from the source and improves the working environment. The system utilizes the principle of low-velocity dilute phase conveying, effectively reducing energy consumption, cutting electricity consumption by more than 30% compared to traditional equipment. The inner wall of the pipeline has been optimized, combined with reasonable elbow arrangement and airflow parameter control, reducing the risk of blockage and improving conveying stability. At the same time, the system is equipped with an intelligent control module that enables automatic start-stop, parameter adjustment, and fault alarms, reducing manual intervention and improving production continuity.
Through the rational application of negative pressure dilute phase technology, this project successfully helped the customer achieve clean, energy-saving, and efficient rubber powder conveyance, earning customer recognition.