

Case Study of Pumping Phosphate Fertilizer Powder Positive Pressure Silo Pumps in Huainan, Anhui
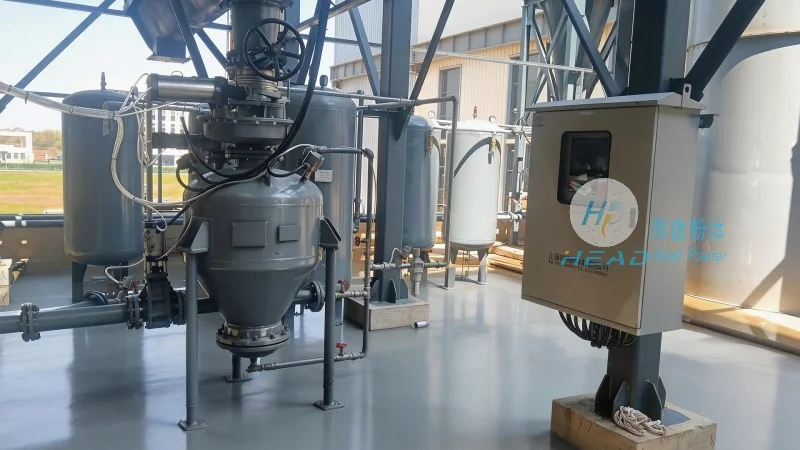
A phosphate fertilizer producer in Huainan, Anhui has long faced challenges such as low conveying efficiency, frequent pipeline blockages, and severe on-site dust pollution during powder transportation. The company processes large quantities of phosphorus fertilizer powder raw materials daily. Traditional mechanical conveying methods not only have high maintenance costs but also cause rapid equipment wear and high energy consumption due to powder characteristics, severely restricting the normal operation of the production line.
Customer pain points
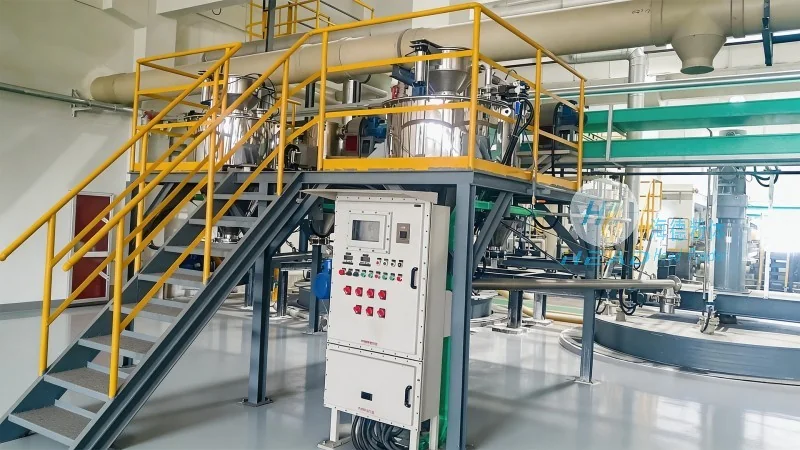
Phosphate fertilizer powder is characterized by high density, easy moisture absorption, and poor flowability. Customers encounter the following core pain points in actual operations:
- Frequent blockages in transportation pipelines require manual cleaning, affecting continuous production;
- Mechanical conveying equipment (such as screw conveyors) suffers severe wear and short maintenance and replacement cycles;
- High dust concentration on site not only affects operator health but also poses safety hazards;
- Traditional conveying methods consume more energy, and operating costs increase year by year.
Product advantages
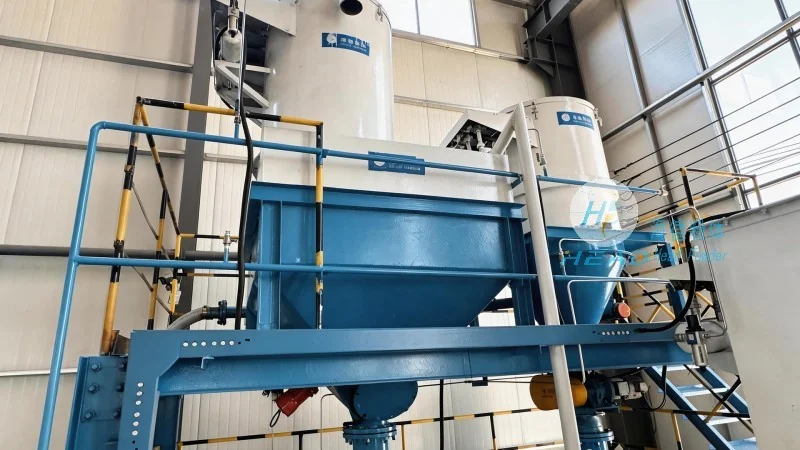
To address these pain points, Head Powder has provided specialized solutions for positive pressure silo pump conveying systems. This system uses compressed air as power to deliver phosphate fertilizer powder to the target location in a high-concentration, low-flow fluidized manner through sealed pipelines, effectively avoiding blockages; At the same time, the fully enclosed pipeline design ensures zero dust leakage, improving the working environment; The system uses wear-resistant elbows and pressure-resistant piping, significantly extending equipment lifespan. In addition, the positive pressure silo pump can flexibly arrange pipelines, adapt to complex workshop layouts, and achieve automated control, reducing manual intervention and reducing overall energy consumption by about 20% compared to traditional solutions.
In the field application in Huainan, Anhui, this solution helped the customer achieve stable all-weather conveying, reducing equipment failure rates by over 60% and improving production continuity. Head Powder continuously provides remote monitoring and regular maintenance services, helping the system operate efficiently over the long term.