

Huzhou Power Plant, Zhejiang Huzhou Power Plant Fly Ash Sealed Storage Complete Set Project
During coal-fired power plant production, the incoming and storage stages of fly ash have long faced practical challenges such as dust leakage, high environmental burdens, and rising labor costs. Head Powder designed a sealed fly ash storage project tailored to the specific working conditions of Zhejiang Huzhou Power Plant, implementing a systematic technical solution to achieve fully closed management of materials from conveyance, warehousing, to storage, effectively reducing dust concentration at the work site, easing environmental protection pressure, and improving storage efficiency and operational stability.
Project Background and Client Pain Points
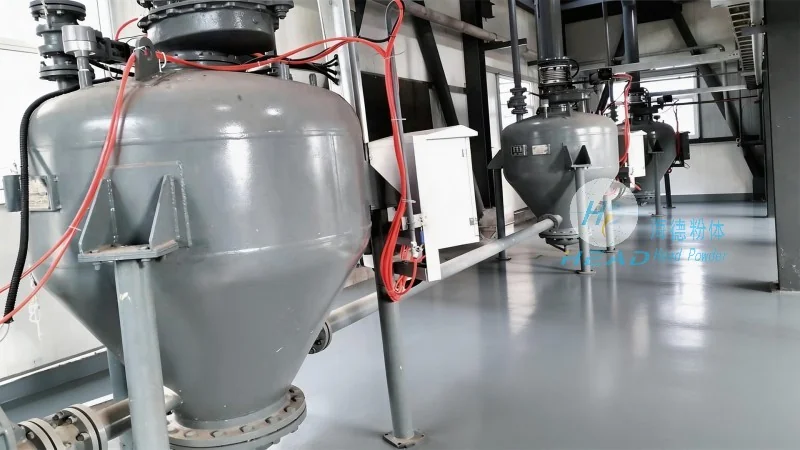
The plant's original fly ash storage methods were open or semi-open, which easily generated dust at the ash outlet and conveying stages, leading to a decline in air quality in surrounding areas and requiring more manual labor for cleaning and dust removal equipment maintenance during daily operations. In addition, open storage areas are prone to damp agglomeration during the rainy season, affecting the quality of fly ash and adversely impacting subsequent comprehensive utilization. Customers urgently needed a warehousing solution that could achieve a fully sealed process, a high degree of automation, and controllable operating costs.
Solutions and product advantages
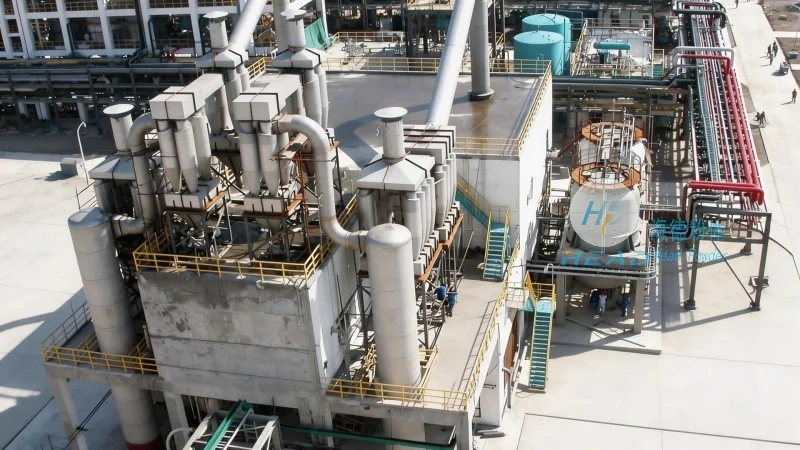
Head Powder integrates a sealed pneumatic conveying system and warehousing design based on on-site conditions. The main technical pathways include:
- Pneumatic conveying system: powered by compressed air, fly ash is directly transported from the ash silo to the sealed storage silo through sealed pipelines, with no leakage points throughout.
- High-efficiency dust removal and filtration: Multi-stage pulse bag dust collectors are installed at the feed inlet, silo top, and exhaust port, helping the dust concentration of the exhaust gas meet environmental protection standards.
- Intelligent control system: Through linkage between the host computer and PLC, automatic adjustment of conveying flow, silo level, and dust collector cleaning cycle is achieved, reducing manual intervention.
- Moisture-proof and anti-caking design: The silo uses an insulated structure and is equipped with a fluidization device to maintain material dryness and support smooth outbound shipment.
After the complete project was put into operation, the dust concentration on site dropped significantly, and the working environment at the posts was noticeably improved; At the same time, due to increased automation, daily inspection and maintenance workload is reduced by about 60%, and overall operating energy consumption is lower than the original method. The sealed warehousing system provided by Head Powder offers reliable technical support for power plants to achieve clean production while reducing costs and increasing efficiency.