

Case Study of Explosion-Proof Sealed Pipeline Transportation of Silicon-Carbon Anode Powder in Suin
In the production of silicon-carbon anode powder, the safety and sealing of the powder conveying stage have always been a focal point of industry concern. To meet the actual needs of a customer in Suining, Sichuan, Head Powder provided an explosion-proof sealed pipeline conveying system, which improved the stability and safety of material transfer, while also reducing the risk of dust spillage.
Case Background
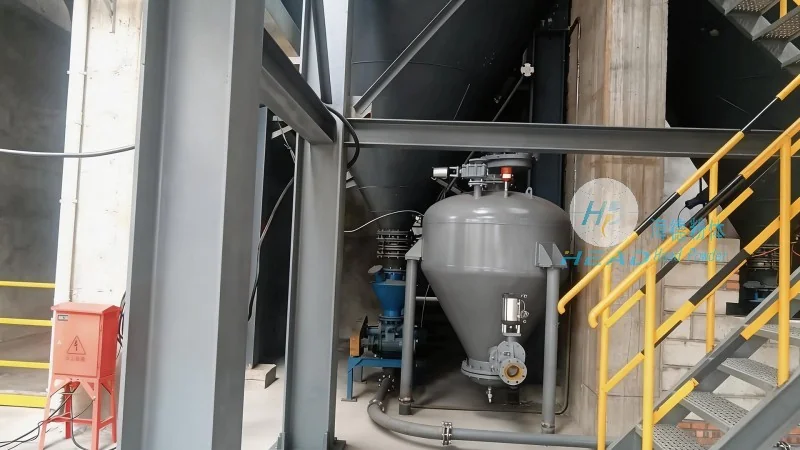
This client is located in Suining, Sichuan, mainly engaged in the production and research and development of silicon-carbon anode materials. As production capacity increases, the original powder conveying methods have gradually revealed issues such as low efficiency, severe dust pollution, and prominent safety hazards. Especially when handling fine-particle, highly active silicon-carbon anode powders, traditional open conveying methods easily trigger dust explosion risks and result in significant material loss.
Customer pain points
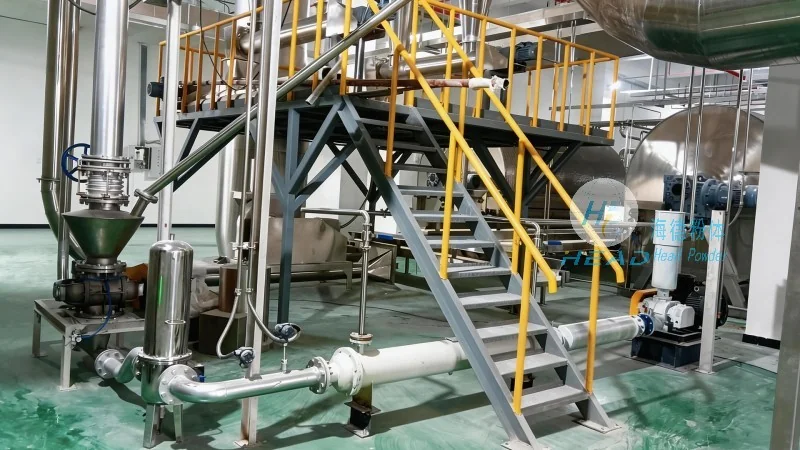
The customer faces multiple practical difficulties during production: First, severe dust generation during powder conveying not only pollutes the production environment but also affects operator health; Second, the open conveying stage poses hidden dangers such as static electricity accumulation and excessive combustible dust concentration, posing high safety risks; Third, materials are prone to moisture and contamination during transportation, causing fluctuations in product quality; Fourth, the existing equipment cannot meet increasingly stringent environmental protection and safety production standards.
Solutions and product advantages
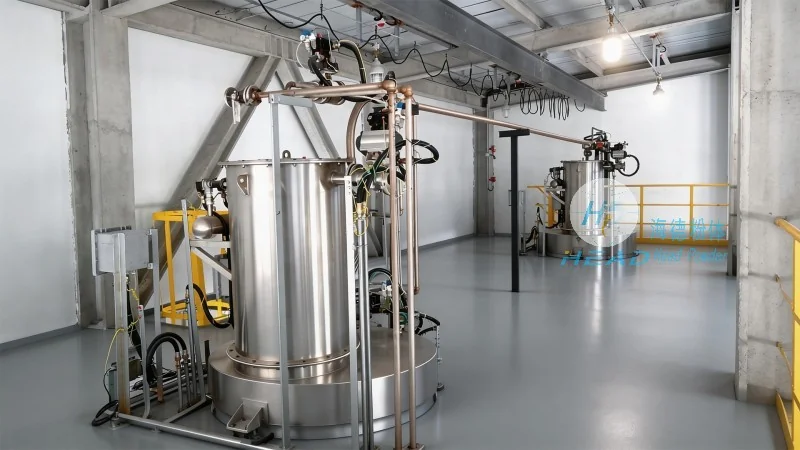
To address these pain points, Head Powder designed and delivered an explosion-proof sealed pipeline conveying system. This system adopts a fully enclosed pipeline structure, combined with nitrogen protection and electrostatic grounding measures, fundamentally eliminating dust leakage and explosion risks. The conveying process uses intelligent control to achieve automatic start-stop, flow regulation, and pressure monitoring, reducing manual intervention and improving operational efficiency. At the same time, the sealed pipeline effectively isolates external moisture and impurities, supporting powder purity and batch stability. The entire set of equipment meets the requirements for explosion-proof area design, helping customers successfully pass safety production inspections.