

Case study of pump conveying desulfurization powder in Lianyungang, Jiangsu
In flue gas desulfurization processes, the stability of the powder conveying system directly affects production operation efficiency. This article combines a case study of a desulfurization project in Lianyungang, Jiangsu, to introduce the practical application of powder silo pump conveying systems, analyze how it solves operational challenges faced by customers, and provide enterprises with reference selection ideas.
Case Summary
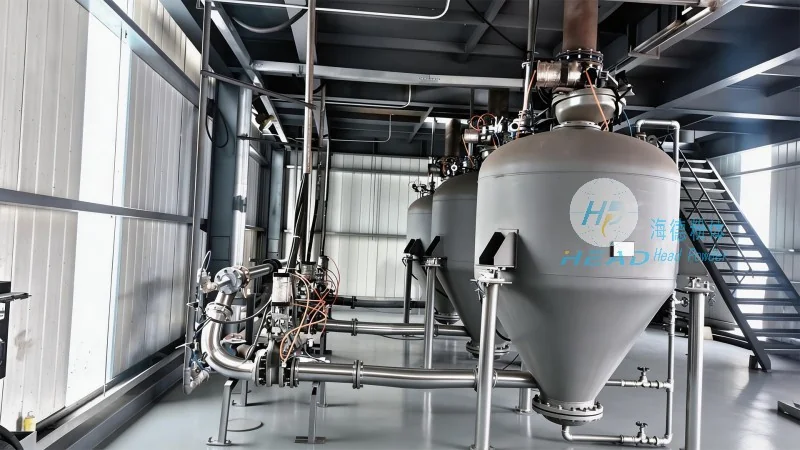
A unit in Lianyungang, Jiangsu, is building a desulfurization unit and needs to transport limestone powder from the powder silo to the reaction zone of the desulfurization tower. Due to site conditions, the conveying distance exceeds 150 meters and must meet multiple unloading requirements. After comprehensive evaluation, the silo pump solution in the pneumatic conveying system was adopted to achieve sealed, continuous, and stable powder conveying.
Customer pain points
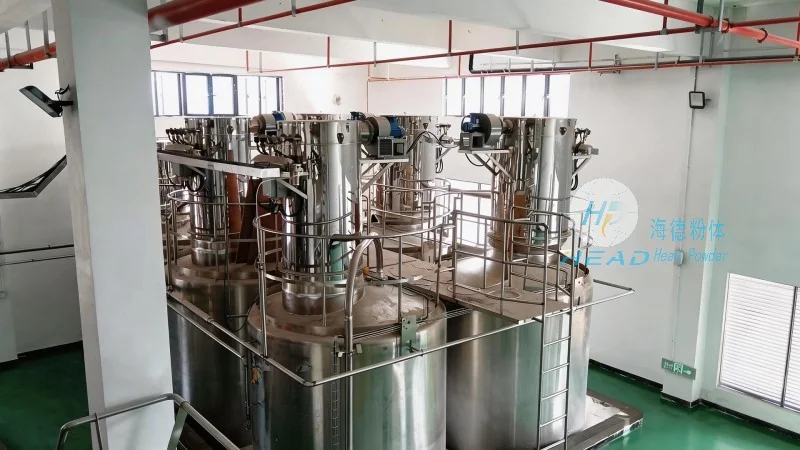
Customers face obvious challenges in the early stages of project planning: first, the conveying distance is long, and traditional mechanical conveying equipment is prone to issues such as belt slippage and dust, resulting in high maintenance costs; Second, powder tends to clump and block pipes, affecting the uniformity of desulfurizer dosing; Third, the on-site environment requirements are strict, requiring dust leakage to avoid and meet environmental emission standards. How to reduce energy consumption and failure rates while improving conveying efficiency has become a core concern for customers.
Product advantages
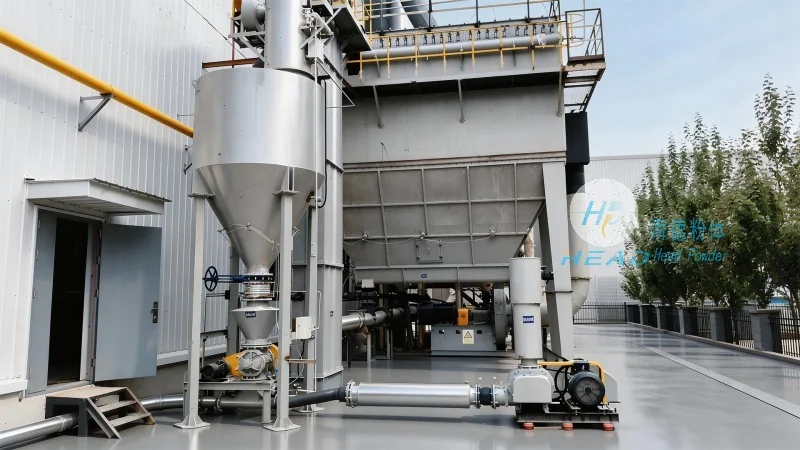
To address these pain points, the company's silo-pump conveying system features the following targeted designs:
- Long-distance stable conveying: Uses the principle of positive pressure pneumatic conveying. By adjusting the flow and pressure of compressed air, powder fluidization can be maintained over distances of over 150 meters, preventing deposition and pipe blockage.
- Low-wear structure: The inner wall of the silo pump and the conveyor elbow are treated with wear-resistant liners to reduce the impact of high-speed powder on metal and extend equipment service life.
- Sealed and environmentally friendly: The entire system uses sealed pipelines combined with pulse baghouse dust collectors to achieve dust-free operation and meet environmental supervision requirements.
- Intelligent control: Equipped with a PLC automatic control system, which automatically starts and stops based on material level signals, and can remotely monitor parameters such as conveying pressure and flow rate, reducing the need for manual intervention.
Actual operational data show that after commissioning, the average daily transport volume of this silo pump system met design requirements, with a failure rate below the industry average, effectively supporting the efficient operation of the desulfurization unit. In the future, similar solutions can be promoted to powder processing in industries such as steel and chemicals.