

Dust-free conveying system for flavor powder in Chengdu, Sichuan
In the flavor powder processing industry, dust dispersion during material transportation is always a key issue affecting the production environment and product quality. A fragrance manufacturer located in Chengdu, Sichuan, has long faced challenges such as severe dust leakage during powder transportation, high raw material waste rates, and substandard workshop cleanliness. Head Powder has developed a custom-made dust-free flavor powder conveying system for them, successfully achieving sealed, low-loss, and highly clean material flow, addressing many pain points caused by traditional conveying methods.
Customer pain points
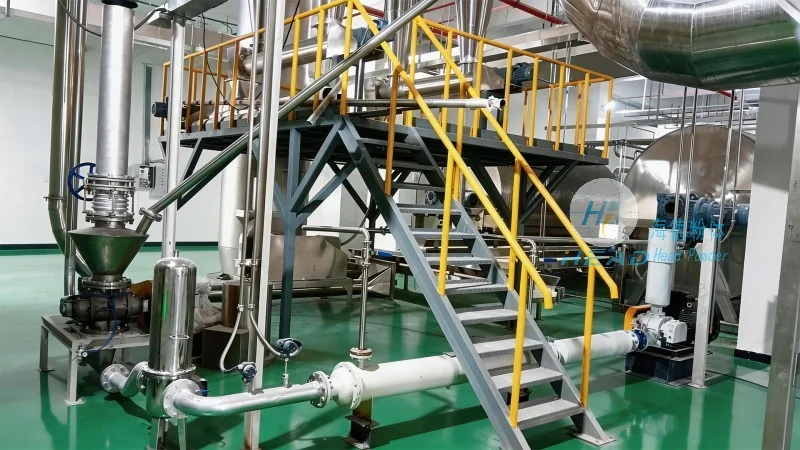
When producing flavor powders, the company's original conveying equipment had the following problems: First, dust was generated during transportation, which not only caused raw material waste but also polluted workshop air and affected employee health; Second, traditional open conveying methods easily cause moisture or cross-contamination of materials, affecting the quality stability of flavors; Third, the process of cleaning and line replacement is long, making it difficult to meet the needs of multi-variety, small-batch production; Fourth, equipment operates with high noise and high maintenance costs.
Product solutions
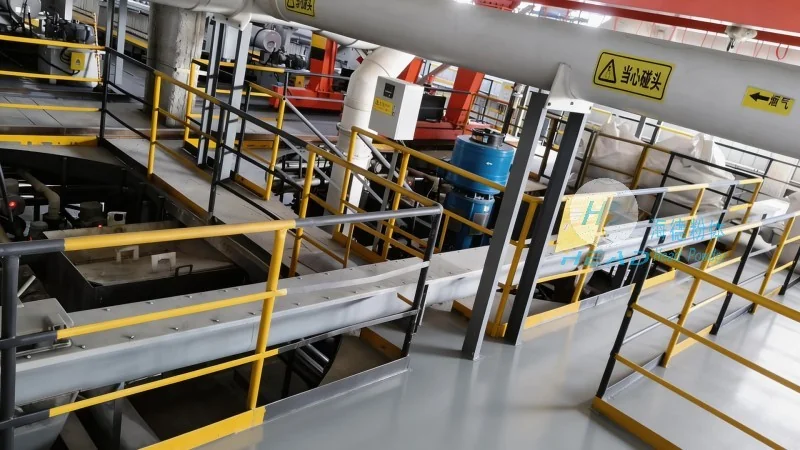
To address these pain points, Head Powder provides a dust-free conveying system for flavor powders in Chengdu, Sichuan. This system uses fully enclosed pipeline negative pressure conveying technology, ensuring dust-free operation from the feeding port to the receiving equipment. Key components such as rotary valves, dust collectors, and pneumatic valves are all made of food-grade stainless steel, meeting hygiene requirements in the fragrance industry. At the same time, the system is equipped with an automatic back-blowing cleaning device and an intelligent control system, allowing the conveying speed to be adjusted according to production cycles, achieving relatively accurate measurement and multi-channel switching. After commissioning, workshop dust concentrations were reduced below safety standards, raw material loss decreased, line switching cleaning times shortened, and overall production efficiency improved.
System operation performance
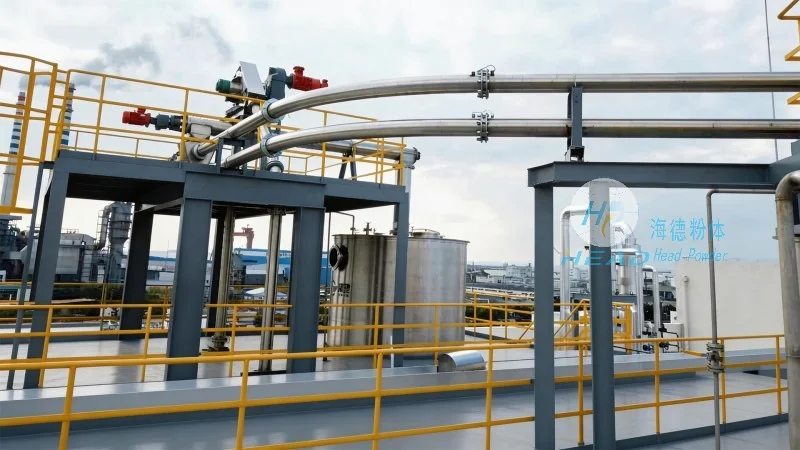
By introducing Head Powder's dust-free conveying system, the company successfully solved two core challenges: dust dispersion and cross-contamination. The recovery rate of raw materials during material transportation has improved, workshop cleanliness meets GMP requirements, and equipment operation is stable. Additionally, the modular design facilitates later expansion and maintenance, leaving room for future capacity upgrades.