

Negative pressure dilute phase conveying project for fine chemical powder in Weifang, Shandong
A fine chemical company's production base in Weifang mainly processes various powdered raw materials, including calcium carbonate, talc powder, titanium dioxide, and others. The original conveying method combined manual feeding with mechanical lifting, which caused issues such as dust overflow, high material loss, and high labor costs. Head Powder designed and implemented a negative pressure dilute-phase pneumatic conveying system for them, achieving sealed, continuous, and automated powder conveying, significantly improving the workshop environment and production efficiency.
Customer pain points
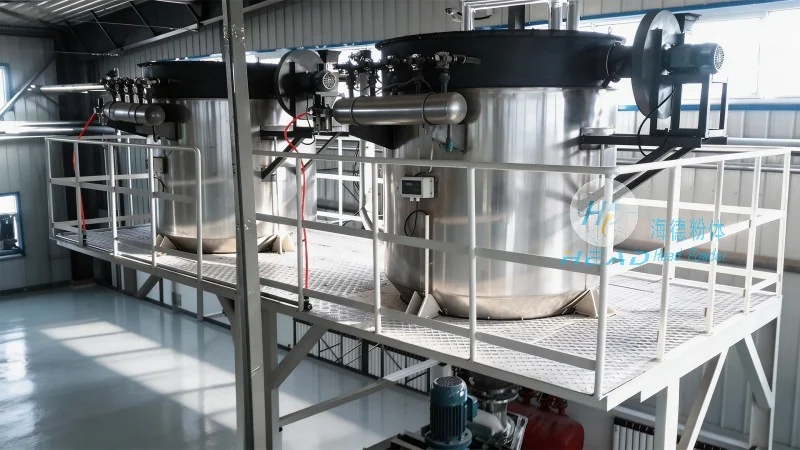
The company faces the following challenges in powder transportation: First, dust generated during traditional conveying not only pollutes the workshop environment but also poses health risks to employees; Second, mechanical lifting equipment easily causes material breakage, affecting product quality; Third, it is difficult to clear material when switching between multiple types of powder, and the process of changing production takes a long time; Fourth, manual handling is inefficient and cannot meet the growing production capacity demand. In addition, frequent maintenance of existing equipment and downtime for maintenance affect production continuity.
Product advantages
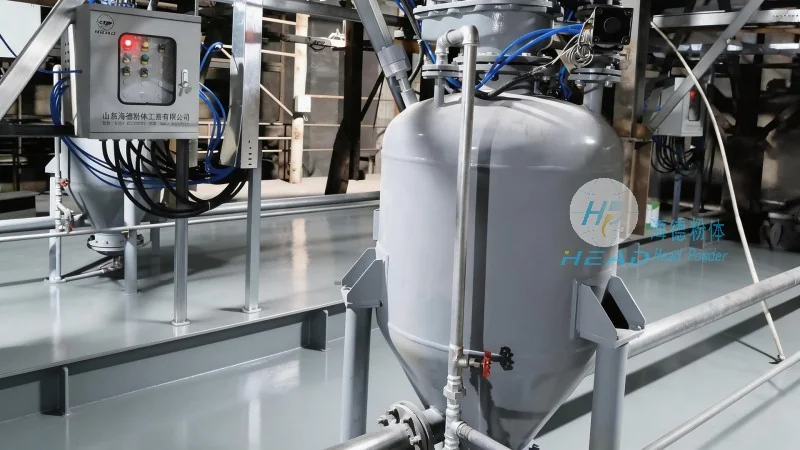
Head Powder addresses customer pain points by providing negative pressure dilute phase conveying solutions. The system uses negative pressure suction, allowing materials to flow at lower wind speeds within the sealed pipeline, effectively reducing material crushing and pipeline wear; Equipped with high-precision dust removal and filtration devices to achieve dust-free emissions; Through the PLC automatic control system, intelligent switching and remote monitoring of multiple nodes and varieties are achieved. This system not only solves dust pollution and material loss issues but also improves conveying efficiency by about 40%, shortens production changeover time by 70%, and reduces labor costs and equipment maintenance frequency.
System features
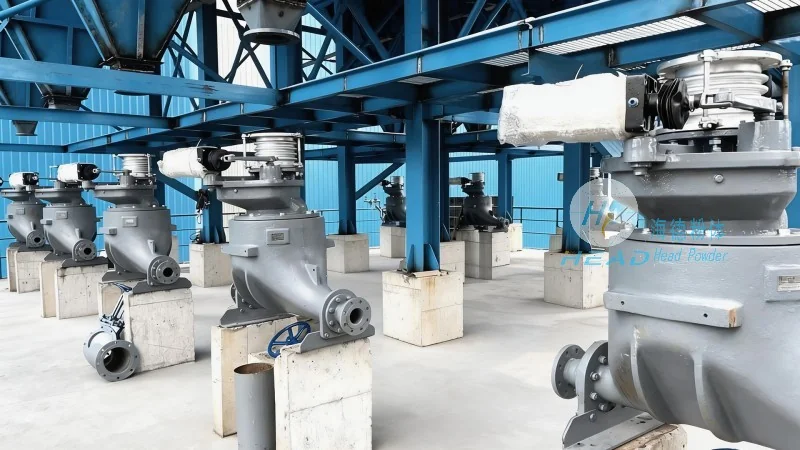
The main features of the negative pressure dilute phase conveying system are low wind speed and high concentration conveying, making it suitable for fine chemical powders with high particle integrity requirements. The sealed piping design prevents material from contacting the outside world, supporting product purity. The system matches conveying speed according to material characteristics, reducing energy consumption while enhancing conveying stability. The modular structure facilitates later expansion and maintenance.