

Shanxi Taiyuan Sugar Powder Anti-Crushing and Conveying Project
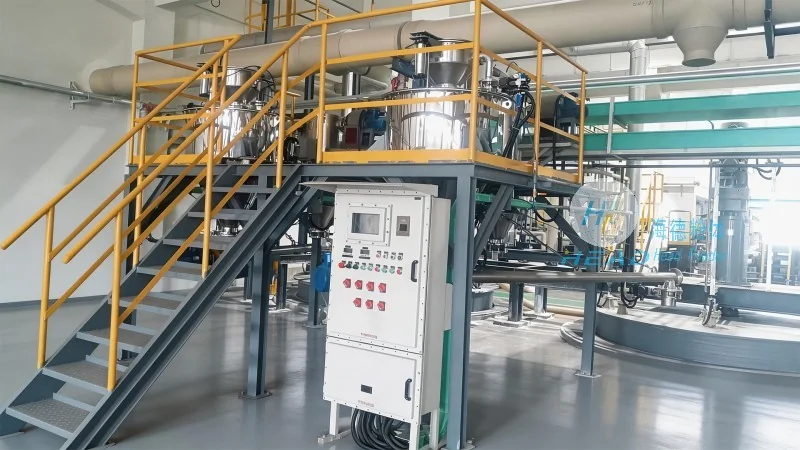
At a sugar powder processing enterprise in Taiyuan, Shanxi, powdered sugar, as a high value-added material, has long faced challenges such as high crushing rates, severe dust emissions, and equipment clogs during transportation. Powdered sugar particles are fine and highly brittle; traditional mechanical conveying methods cause large amounts of crushing, resulting in loss of product value; At the same time, the spillage of fine powder causes environmental problems in the workshop and increases subsequent cleaning costs. The client wanted to find an engineering solution that could effectively reduce the crushing rate while achieving sealed, dust-free, and continuous conveying.
Professional solutions
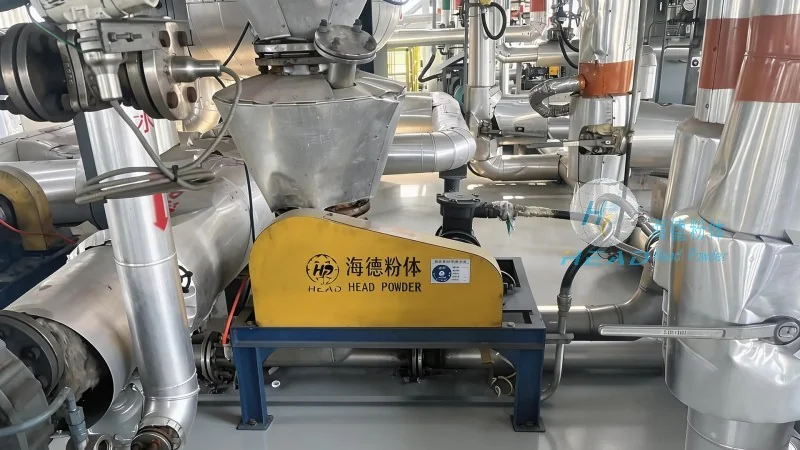
To address the characteristics of sugar powder being easily crushed and dusty, Head Powder customized an anti-crushing pneumatic conveying system for the company. The system adopts the principle of low-pressure dense phase conveying, precisely controlling airflow velocity and material-gas ratio, allowing powdered sugar to move at low speed and high concentration within the pipeline, fundamentally reducing particle collisions and friction on the pipe walls. The interior of the conveying pipeline is specially polished and equipped with multiple buffer elbows to further reduce impact force. Adding flexible connecting devices and anti-crush valves at key points helps ensure smooth material flow. The entire system operates in a fully enclosed manner, with a high-precision dust removal and filtration device at the rear end, achieving zero dust leakage.
Application Effectiveness and Value
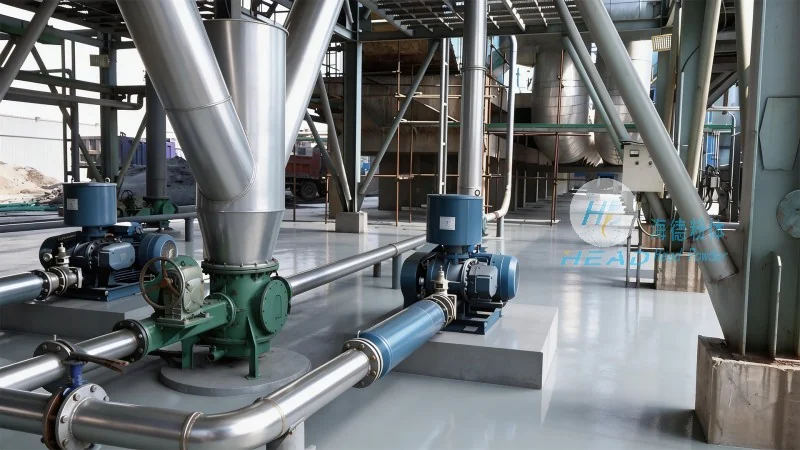
After the project was put into use, the crushing rate of sugar powder was reduced by more than 80% compared to traditional methods, and the product particle integrity was improved. The workshop environment has significantly improved, with dust concentrations dropping below health and safety standards. At the same time, conveying efficiency is stable, system maintenance cycles are extended, and overall operating costs are significantly reduced. This solution helps customers achieve the dual goals of clean production and energy savings while contributing to quality.