

Guangxi Liuzhou Ultrafine Mineral Powder Positive Pressure Silo Pump Transmission Project
At an ultrafine mineral powder processing project in Liuzhou, Guangxi, the company faces the challenge of long-distance, high-concentration transportation of powdered materials. A company commissioned our company (Head Powder) to design and implement a positive pressure silo pump delivery system for them, designed to stably transport ultrafine mineral powder from the storage silo to downstream sections. After the project was put into operation, conveying efficiency improved, the system operated stably and reliably, and received high recognition from customers.
Customer pain points
The customer's original conveying method combined simple mechanical and manual handling, with the following prominent issues: First, severe dust emissions and harsh working environment pose health threats to operators; Second, the material loss rate during conveying is high, resulting in significant energy consumption; Third, frequent equipment maintenance and long downtime for repairs affect overall production efficiency; Fourth, it is impossible to achieve automated continuous conveying, making it hard to match the cycle time requirements of subsequent processes.
Product advantages
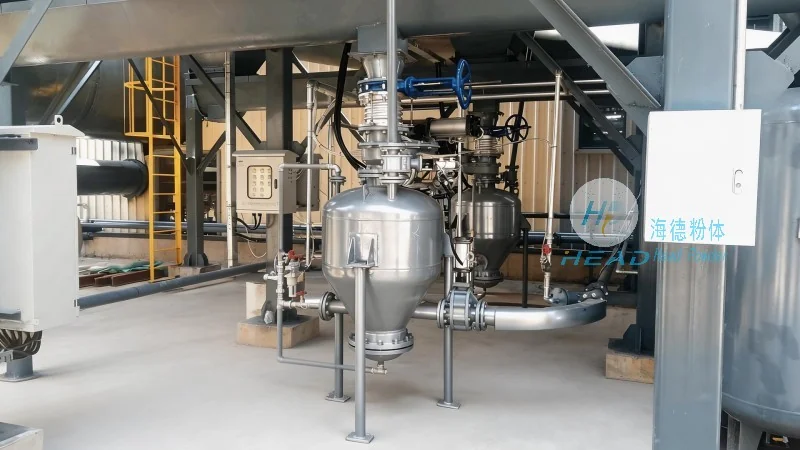
To address these pain points, Head Powder provides a positive pressure silo pump conveying system as a solution. This system uses compressed air as the power source, and materials are conveyed in a dense-phase fluidized manner inside sealed pipelines, fully preventing dust leakage. Through optimized gas-solid ratio control and intelligent valve regulating valve groups, energy consumption is reduced by about 30% compared to traditional methods. The system is equipped with a fully automatic PLC control system, supporting remote monitoring and fault warning, which reduces manual intervention and maintenance workload. At the same time, pipes and elbows are made of highly wear-resistant materials, extending service life and reducing the frequency of spare parts replacement.
Product features
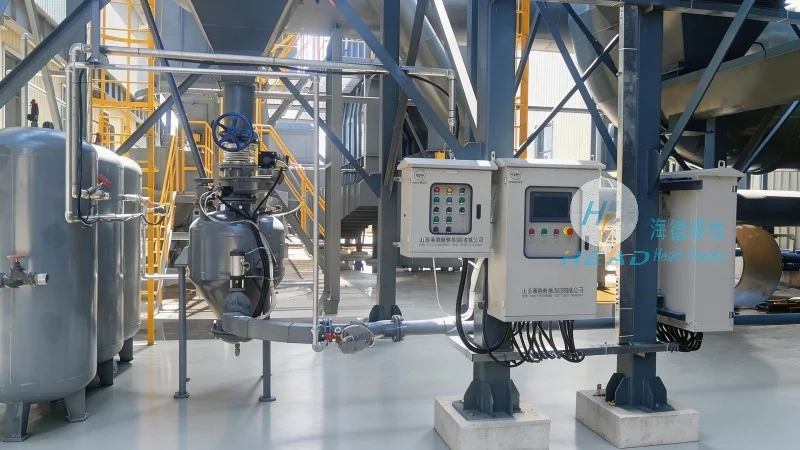
- Closed conveying: Fully enclosed pipeline structure, no dust leakage, meeting environmental protection and occupational health requirements.
- Low energy consumption operation: Uses low-pressure dense phase conveying technology, with a reasonable gas-to-material ratio, and overall energy consumption lower than traditional dilute-phase conveying.
- Intelligent control system:P LC automation control, supporting multi-mode switching and remote communication, allowing seamless integration with factory MES systems.
- High wear-resistant structure: Pipeline lining and elbows are made of ceramic or alloy materials, suitable for the high wear characteristics of ultrafine mineral powder, resulting in a long service life.
Product specifications
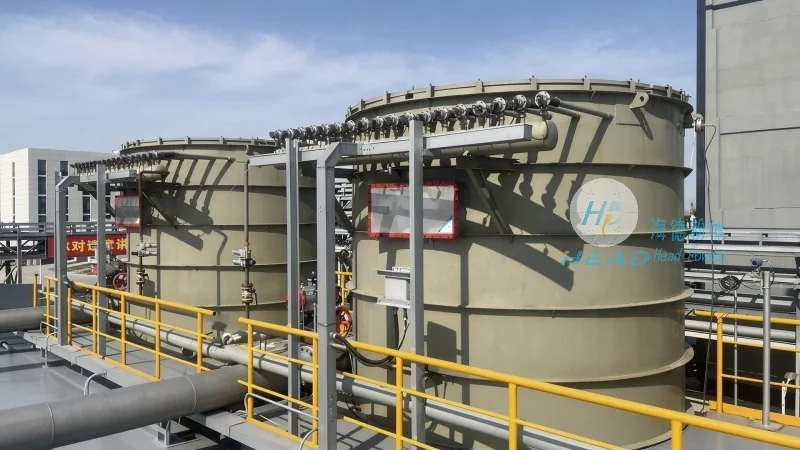
- Conveying capacity: 5~50 t/h (customized according to different working conditions)
- Work pressure: 0.2~0.6 MPa (low-voltage dense phase)
- Conveying distance: Horizontal ≤ 500 m, vertical ≤ 50 m (expandable)
- Air source requirements: Compressed air flow ≥ corresponding value, oil content ≤ 0.1 ppm