

Inner Mongolia Tongliao Metal Powder Sealed Explosion-Proof Engineering Project
In the field of metal powder processing, the risk of dust explosions has long been a challenge for industry safety production. A metal powder processing company in Tongliao, Inner Mongolia, faces severe explosion-proof safety challenges due to hidden dangers such as dust accumulation, static electricity release, and insufficient equipment sealing on its production line.
Case Summary
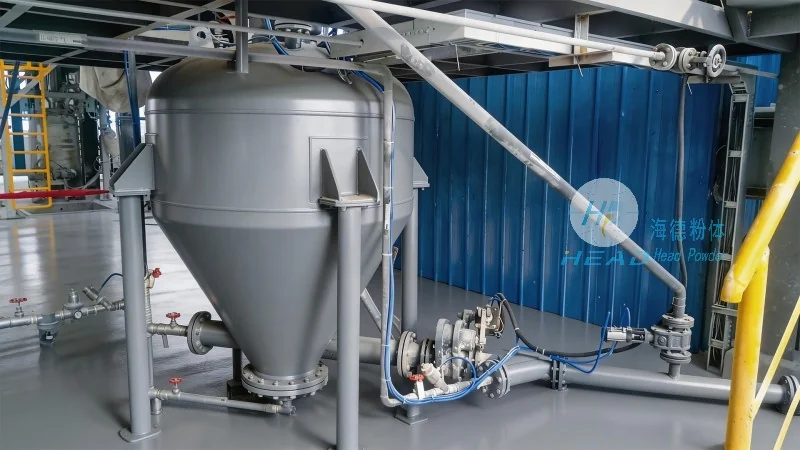
A metal powder processing company located in Tongliao, Inner Mongolia, mainly produces aluminum powder, magnesium powder, and other flammable and explosive metal powders. The original production line lacked systematic explosion-proof design, with dust concentrations in the workshop frequently exceeding standards, poor equipment sealing, and the risk of static sparks ignition. Multiple minor flash explosions led to production stoppages for rectification.
Customer pain points
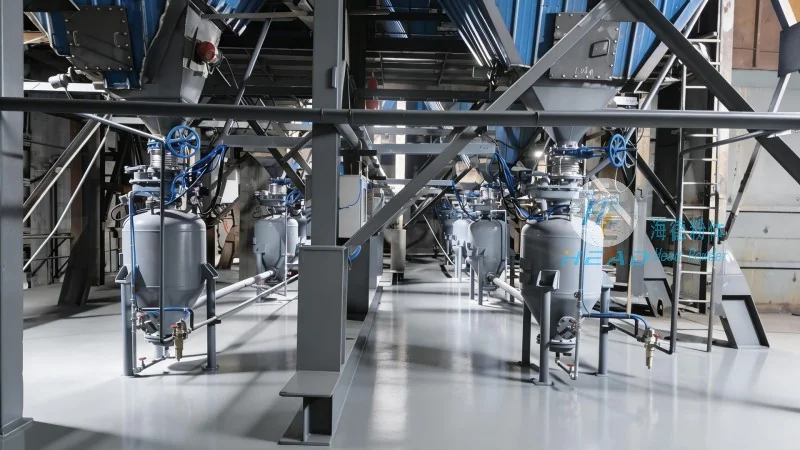
Enterprises face three core pain points: First, metal dust during production is prone to leakage, creating an explosive suspended environment; Second, existing equipment lacks reliable inert gas protection and explosion suppression functions; Third, there is a lack of intelligent monitoring and emergency response systems, making real-time early warning and automatic intervention impossible. In addition, local safety regulatory authorities have strict requirements for explosion-proof ratings, so companies need to upgrade compliance as soon as possible.
Product advantages
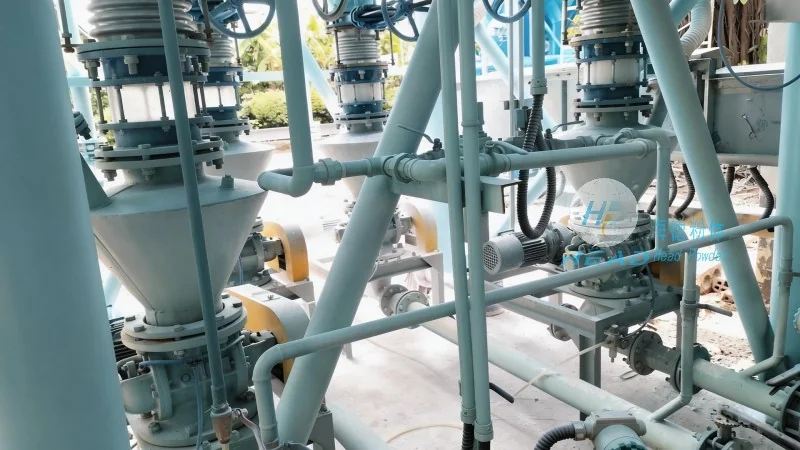
To address these pain points, Head Powder offers an integrated sealed explosion-proof engineering solution. This solution uses a highly sealed explosion-proof enclosure paired with an automatic nitrogen displacement system, ensuring that the oxygen content inside the equipment is stably controlled below the lower explosive limit; At the same time, multi-point pressure sensors and quick-response explosion suppression devices are deployed to achieve millisecond-level suppression in the early stages of explosions; Additionally, it is equipped with static grounding monitoring, real-time dust concentration alarms, and a remote intelligent control platform to help enterprises achieve unmanned safe operations. The entire system has passed national explosion-proof certification and features a modular design that facilitates on-site modification and maintenance.