

A case study of dilute phase negative pressure conveying of nanopowders in Mianyang, Sichuan
A nano powder manufacturer in Mianyang, Sichuan faces issues such as low fine powder conveying efficiency, severe dust pollution, and rapid equipment wear during production. To address these pain points, Head Powder offers a dilute-phase negative pressure conveying system, achieving sealed, efficient, and low-energy nano-level powder delivery, significantly improving the production environment and reducing operating costs.
Case Summary
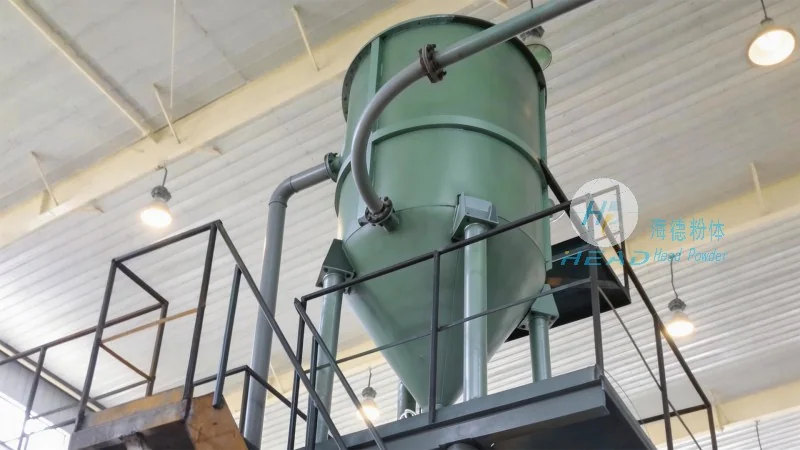
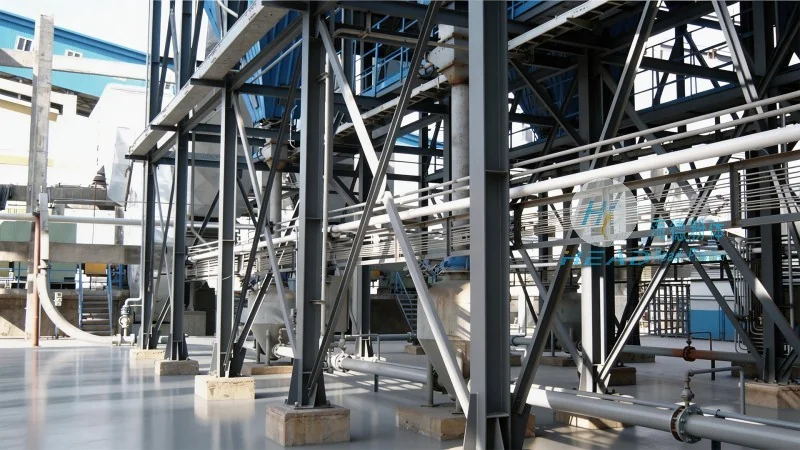
The company mainly produces nano alumina powder, with raw material particle sizes ranging from 50~200 nanometers, characterized by high added value, easy dust generation, and poor flowability. The original manual feeding + mechanical lifting method resulted in high material loss, harsh working conditions, and frequent replacements resulting in prolonged downtime. Head Powder designed a dilute-phase negative pressure pneumatic conveying system for it, enabling relatively accurate delivery from the storage silo to multiple mixing tanks, with fully sealed operation with no leakage or blockages.
Customer pain points
- During traditional transportation, nano powders tend to generate static electricity and agglomerate, leading to pipeline blockages and affecting production continuity.
- Severe dust dispersion does not meet environmental protection requirements and endangers operator health.
- Manual transfer and intermittent operations result in low overall efficiency and cannot meet the needs of capacity expansion.
- Equipment wears out quickly, maintenance costs are high, and annual downtime exceeds 40 days.
Product advantages
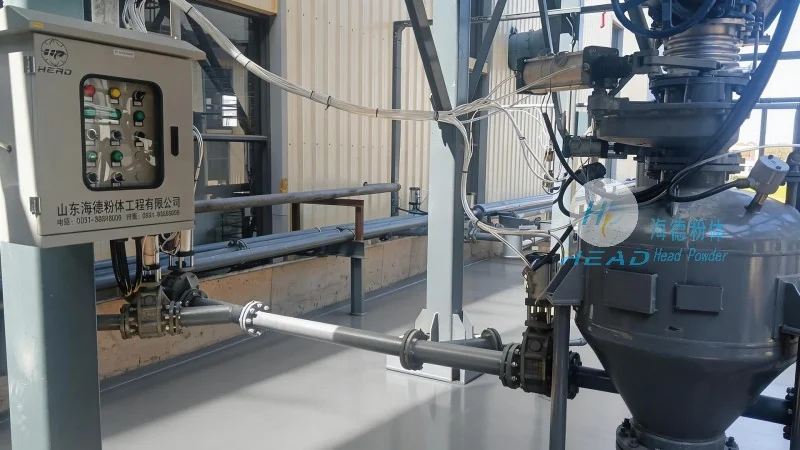
To address these pain points, Head Powder's dilute-phase negative pressure conveying solution has the following main features:
- Sealed negative pressure conveying: The system uses negative pressure suction and control, with adjustable gas flow rate inside the pipeline, fully preventing dust leakage and reducing on-site dust concentration to below 2mg/m³.
- Anti-clustering and anti-clogging design: Equipped with dedicated fluidization devices and anti-static pipeline linings, combined with pulse back-blowing systems, effectively preventing nano powder deposits at elbows and pipe walls, facilitating continuous normal operation.
- Intelligent control system: Integrates PLC and touchscreen to achieve automatic start/stop, fault alarms, and accurate multi-station batching. The user interface is intuitive and can be integrated into the factory's MES system.
- Low energy consumption and long lifespan: Optimized fan selection and pipeline routing, reducing unit energy consumption by 30% compared to traditional mechanical conveying; Wear-resistant elbows and quick-release clamp design extend replacement intervals to over 12 months.
After the system was put into operation, the client's production capacity increased by 25%, annual maintenance costs dropped by 60%, and the workshop environment met food-grade cleanliness standards, becoming a benchmark project for nano powder conveying in Sichuan.