

Example of Baking Soda Powder Silo Pump Conveying in Ningbo, Zhejiang
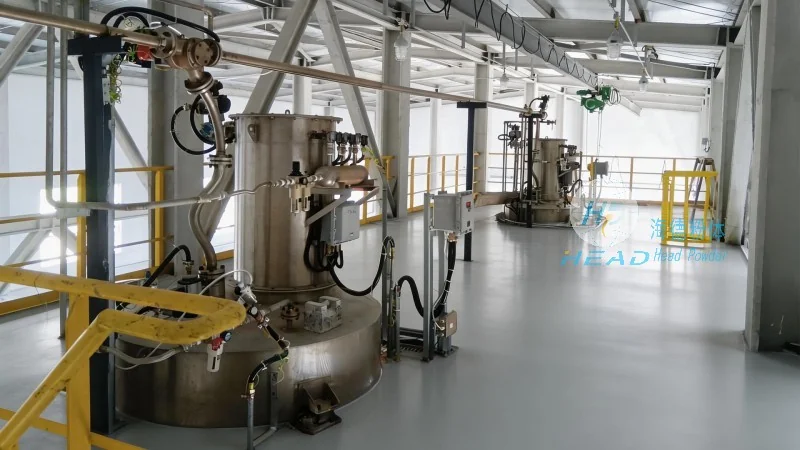
A company located in Ningbo, Zhejiang, mainly produces and stores baking soda powder. The company faced issues such as the baking soda powder easily clumping during transportation, severe dust generation, and limited conveying distance, which affected production efficiency and the on-site environment. After extensive comparison, the final adoption of the silo pump conveying system provided by Head Powder achieved sealed, efficient, and stable delivery of baking soda powder.
Customer pain points
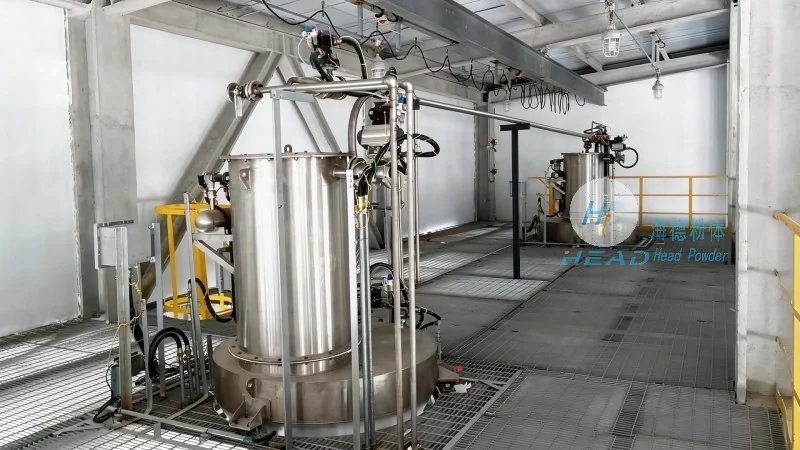
Baking soda powder has slight hygroscopicity and is prone to flying. Traditional mechanical conveying methods have three prominent issues: first, powder tends to adhere to the inner walls of conveying pipes, leading to blockages and reduced production capacity; Second, open conveying causes large amounts of dust to leak, polluting the workshop environment and increasing cleaning costs; Third, insufficient pressure during long-distance conveying, unable to meet the material needs of multiple stations. The customer urgently needed a pneumatic conveying solution that could solve the above issues, was reliable to operate, and easy to maintain.
Product advantages
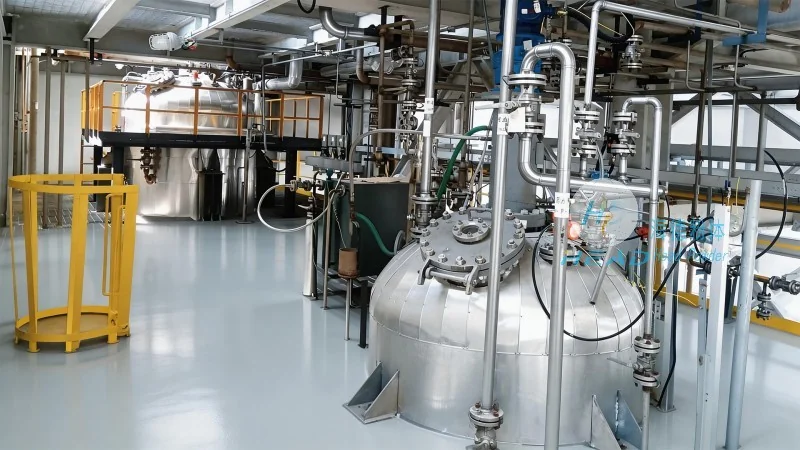
To address customer pain points, Head Powder has launched a customized baking soda powder silo pump conveying system, offering the following advantages:
Sealed transport with no dust leakage: The silo pump system adopts a fully enclosed pipeline structure, isolating materials from the outside world throughout transportation, eliminating dust at the source and improving workshop air quality.
Anti-stick and anti-blockage design: Based on the characteristics of baking soda powder, the silo pump fluidization device and pipeline inner wall treatment process have been optimized to reduce material adhesion, facilitate smooth transportation, and lower downtime and cleaning frequency.
Long-distance stable conveying: By reasonably configuring air source pressure and silo pump volume, stable horizontal and vertical transport spanning hundreds of meters is achieved, meeting the allocation needs of multiple stations and multiple silos.
Automated control makes operation convenient: The system is equipped with a PLC intelligent control module that can remotely monitor conveying pressure, material level, and operating status, reducing manual intervention and improving overall efficiency.
After this solution was put into operation, the customer's baking soda powder conveying efficiency improved by about 30%, on-site dust concentration dropped significantly, equipment maintenance costs were lowered, and it was well received by users.