

Guangxi Hezhou phosphorus chemical powder sealed conveying project
In the phosphorus chemical production process, the conveying stage of powdered materials often faces challenges such as dust leakage, material loss, and frequent equipment maintenance. A large phosphorus chemical enterprise in Hezhou, Guangxi, has introduced a specialized pneumatic conveying system for its sealed powder conveying project in Hezhou, Guangxi, specifically to address these pain points. This project achieves efficient and environmentally friendly material transfer through a fully sealed, automated conveying solution, providing a practical example for the industry.
Customer pain points
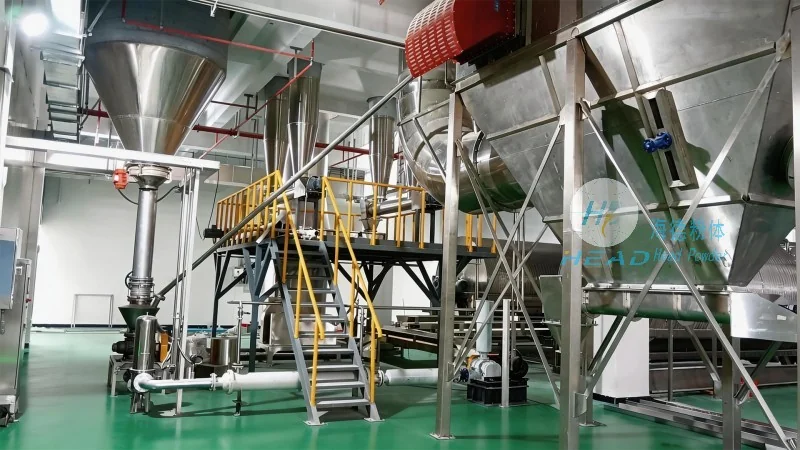
During production, the company originally used an open belt conveyor combined with manual transfer for powder conveying, resulting in the following prominent issues:
- Severe dust pollution:Phosphorus chemical powder particles are fine and easily flying; open conveying causes excessive dust concentrations in workshops, affecting employee health and increasing environmental management costs;
- High material loss:During transfer, material leakage and scattering lead to high loss rates, directly increasing production costs;
- High maintenance frequency:Equipment such as belt conveyors is prone to wear and material blockages, frequent shutdowns for maintenance, and affect continuous production;
- High energy and labor costs:Multi-stage transfers require multiple operators to supervise on site, and the equipment operates with low efficiency and high power consumption.
Product advantages
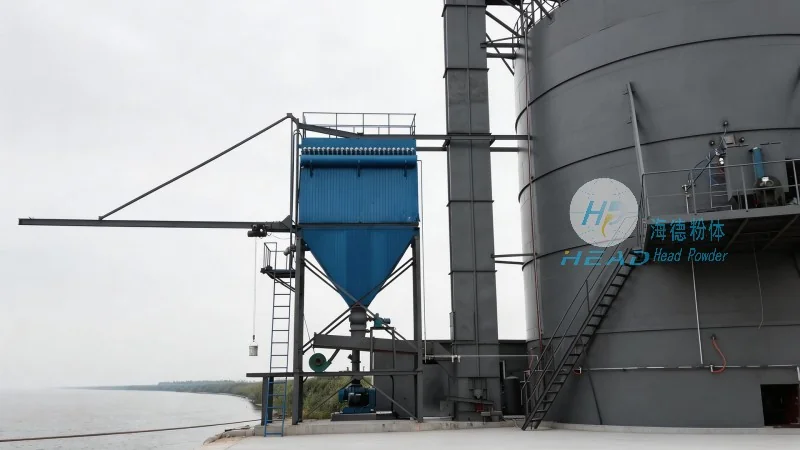
To address these pain points, Head Powder has customized a sealed pneumatic conveying system for the company, with main features including:
- Fully enclosed conveying, zero dust leakage:Uses positive pressure pneumatic conveying, with pipelines fully sealed, allowing materials to be transported in negative or positive pressure airflow, eliminating dust leakage at the source, significantly improving the workshop environment, and meeting strict environmental protection requirements;
- Low Loss, High Efficiency:The system uses precise airflow control and sealing design, resulting in material conveying loss rates below 0.1%, while improving conveying efficiency by more than 30% compared to traditional methods;
- Intelligent control reduces manual labor:Equipped with a PLC automatic control system that monitors pressure, flow, and material level parameters in real time, enabling one-click start-stop and remote monitoring, reducing the need for on-site operators;
- Durable equipment and easy maintenance:Key components use wear-resistant materials, with optimized design of bends and valves to extend equipment lifespan, reduce daily maintenance workload, and support normal production line operation.
Currently, the project has been operating normally for over 12 months. Customers report dust emission concentrations below national limit standards, material loss rates have dropped to within 0.05%, comprehensive energy consumption has decreased by about 20%, and operation and maintenance costs have been reduced by 35%. This successful application further validates the feasibility of the sealed pneumatic conveying solution in the phosphorus chemical industry and provides reliable technical reference for similar enterprises.